Negative turning inserts
ISO negative carbide inserts (NST) — nine chip grooves from finishing to roughing in steel, stainless and cast iron.
Galtona's NST range is the widest negative-turning program, with nine dedicated chip grooves for finishing through roughing.
For steel: SWX+ (Masterfinish, high surface quality), WL+ (light finishing), WM+ — the broadest range, spanning 7 insert shapes across GTCP115, GTCP125, GTCP125HP, GTCP135, and cast-iron GTCK120 — and WR+ for medium roughing.
For stainless and exotic materials: JF (cermet finishing), EXK+ (CNGP/DNGP/VNGP/WNGP finishing), IPK+ (new chipbreaker, low cutting forces), and IPR+ (medium machining and light roughing).
For cast iron roughing: 909+, available in coated-carbide GTCK120/GTCK110HP, including flat-top (no-chipbreaker) …-EN inserts rated for interrupted cuts.
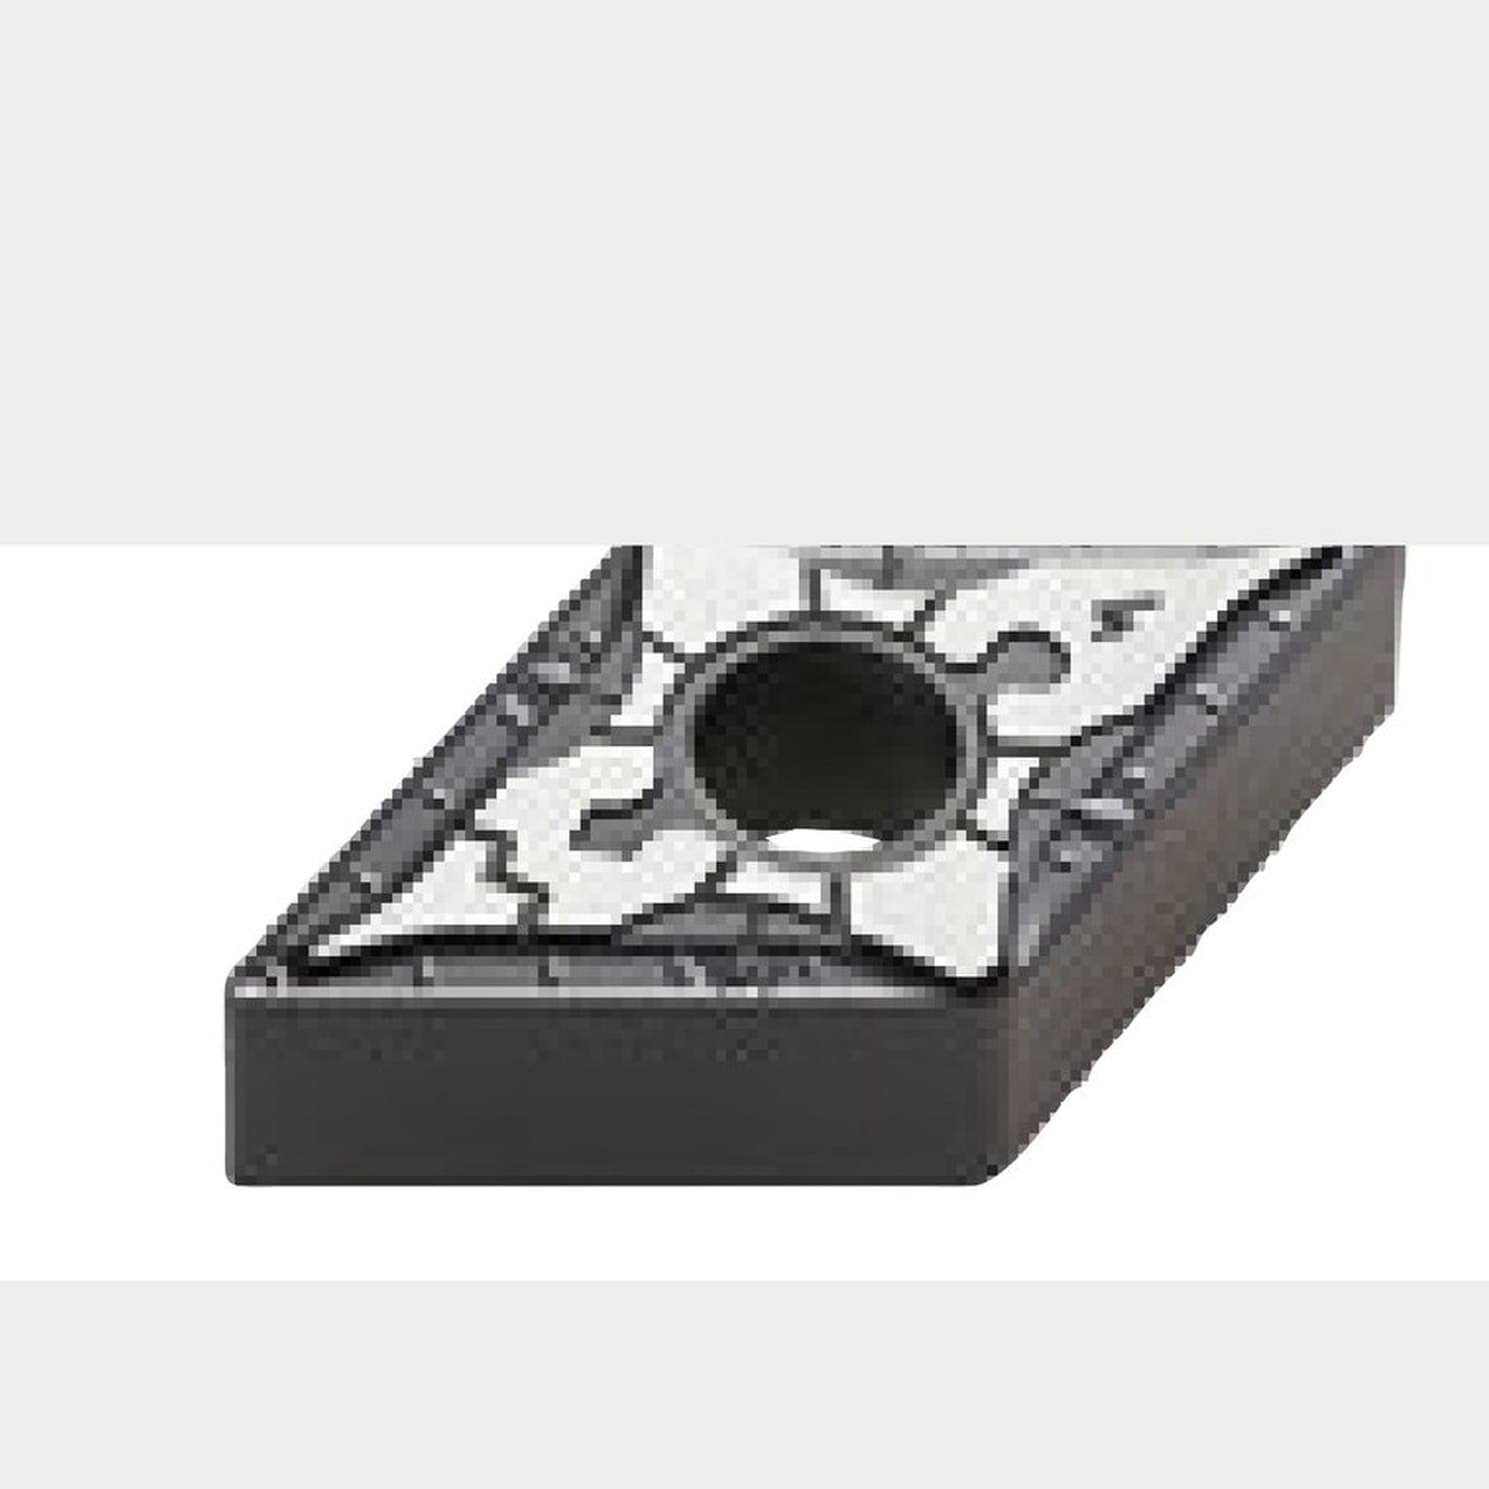
SWX+ — Masterfinish finishing
SWX+ — Masterfinish Finishing
FEM-optimised Masterfinish geometry for high surface quality, steel "P15".
Example: CNMX 120408-SWX+. Depth of cut 0.50–3.00 mm, feed 0.35–0.15 mm.
Swipe to see more →
| Designation | Chipbreaker | Material No. | Available |
|---|---|---|---|
| CNMX 120404-SWX+ GTCP115 | …-SWX+ | MM12078117 | ● |
| CNMX 120408-SWX+ GTCP115 | …-SWX+ | MM12078114 | ● |
| DNMX 150604-SWX+ GTCP115 | …-SWX+ | MM12078116 | ● |
| DNMX 150608-SWX+ GTCP115 | …-SWX+ | MM12078110 | ● |
| WNMX 080404-SWX+ GTCP115 | …-SWX+ | MM12078112 | ● |
| WNMX 080408-SWX+ GTCP115 | …-SWX+ | MM12078109 | ● |
Cutting data — general cutting parameters by workpiece material
Swipe to see more →
| Group | Type / alloy | Hardness HB | GTCP115 vc | GTCP125 vc | GTCP135 vc |
|---|---|---|---|---|---|
| P | Non-alloyed steel 0–0.45% C | 150–250 | 220–400 | 170–240 | 170–190 |
| P | Low-alloyed steel | 250–300 | 200–320 | 100–190 | 90–150 |
| P | High-alloyed steel | 200 | 180–320 | 130–210 | 120–200 |
| P | Corrosion-resistant steel | 200 | 200–320 | 130–210 | 140–180 |
| M | Ferritic stainless | 200 | 220–320 | 140–210 | 140–200 |
| M | Austenitic stainless | 180 | – | 100–210 | 110–190 |
| M | Duplex stainless | 230–260 | – | – | 80–150 |
| M | Martensitic stainless | 330 | – | 70–100 | 55–75 |
| K | Grey cast iron | 180 | 140–370 | 130–210 | – |
| K | Spheroidal cast iron | 160 | 190–430 | 120–240 | – |
| K | Malleable/tempered iron | 130 | 180–520 | 150–250 | – |
Rated for consistent and inconsistent cutting depth; not for interrupted cuts.