Multicut 4-in-1 indexable drilling, boring and turning tool
A 4-in-1 cutting tool for drilling, boring and turning — one indexable drill-turn system, Ø8.00–32.00 mm.
One tool. Four operations. Zero compromise.
MULTICUT turns drilling, boring, face turning, and external turning into a single indexable insert system — Ø8.00–32.00 mm, 1.5×D or 2.25×D deep, with true flat-bottom holes straight into solid material. No tool changes. No compromises.
One holder, two insert families: XPNT for general-purpose work, XPET for aluminium. Less programming, fewer tools and inserts to stock, real savings on acquisition, faster set-up — all from day one.
Four coated grades — GTCP425, GTCP435, GTPP430, and GTWN715 for aluminium — span the full ISO range (P, M, K, N, S). Optimised stability, Torx Plus clamping, and hard-and-tough surfaces keep every insert locked down and every chip moving, shift after shift.
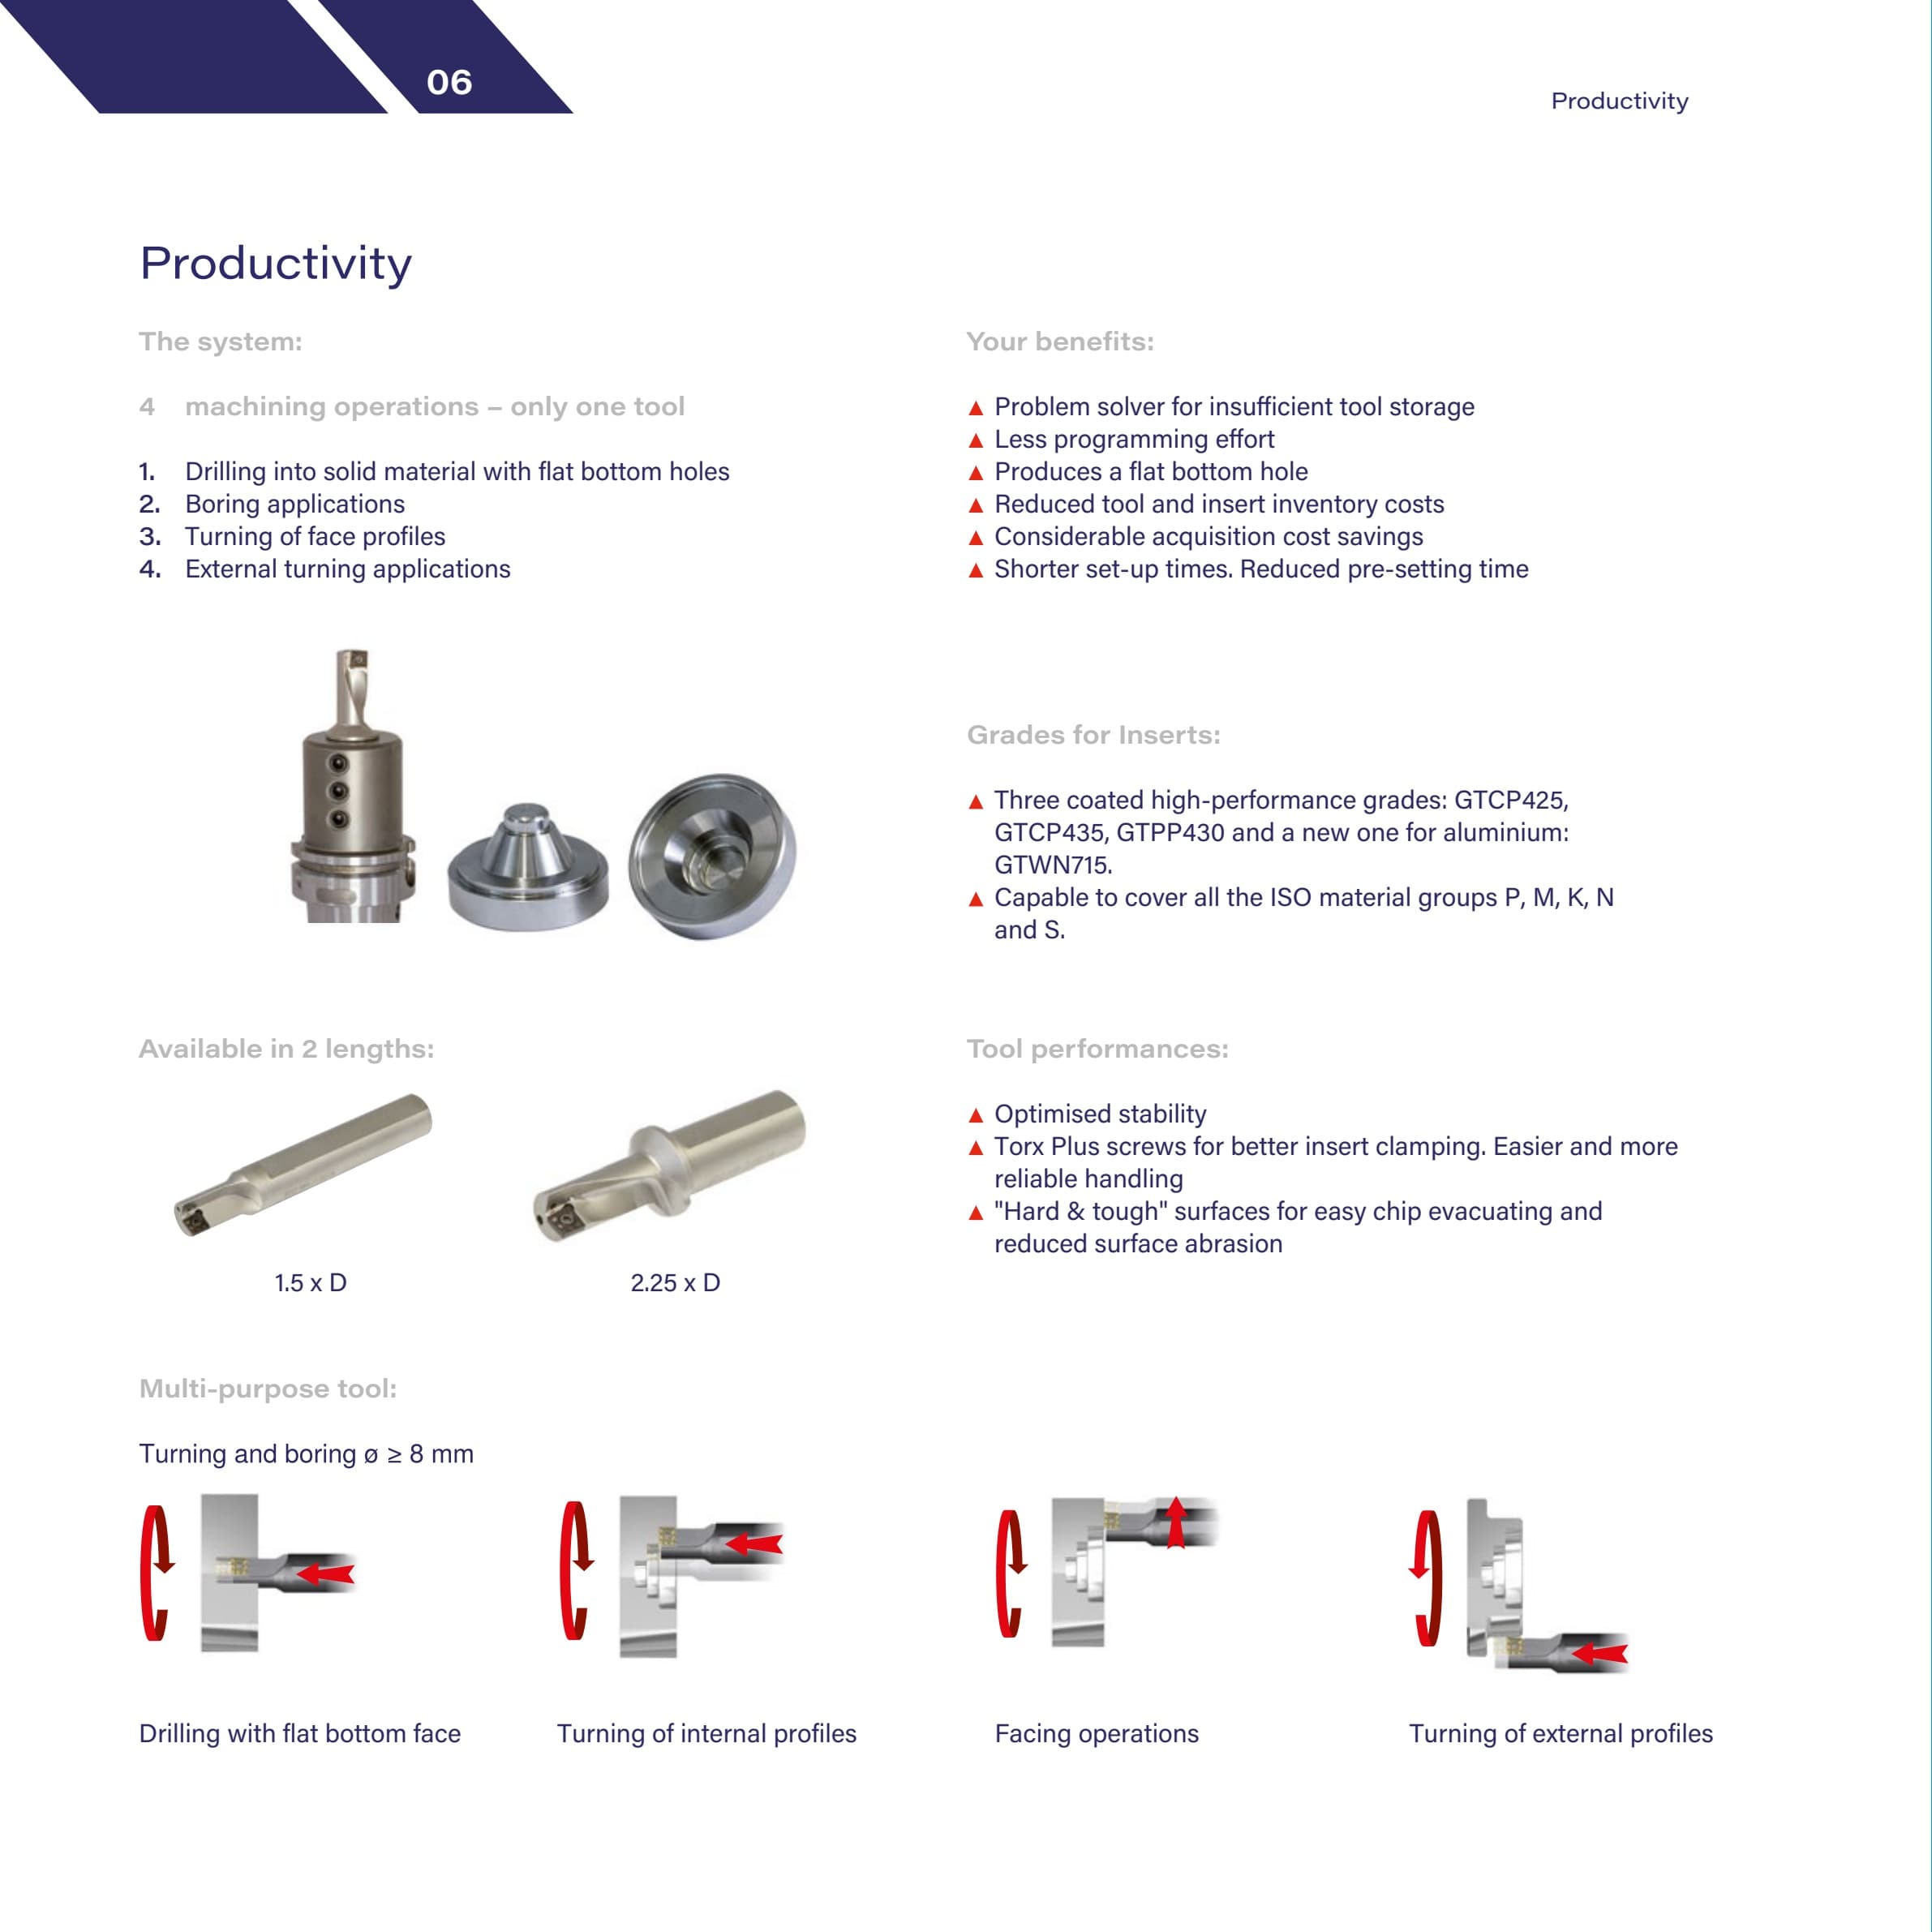
4 operations, 1 tool — GTCP425, GTCP435, GTPP430 & GTWN715 grades, ISO P/M/K/N/S, 1.5×D and 2.25×D
Insert Grades
Coated high-performance grades, covering ISO material groups P, M, K, N, and S.
GTCP425 (HC-P25 | HC-K30 | HC-M20)
Co 7.0%; mixed carbides 8.1%; WC balance. Grain size 1–2 μm. Hardness HV30 1450. Coating: CVD Ti(CN)₂O₃Al multi-layer. Wear-resistant solution for steel and cast iron under stable conditions with high cutting speed.
GTPP430 (HC-P30 | HC-M25 | HC-S25 | HC-K30 | HC-N25)
Co 9.0%; others 0.75%; WC balance. Grain size 0.85 μm. Hardness HV30 1590. Coating: PVD TiAlN. Universal high-performance grade for steel, austenitic steel, and heat-resistant alloys.
GTCP435 (HC-P35 | HC-K40 | HC-M30)
Co 9.6%; mixed carbides 7.8%; others 0.4%; WC balance. Grain size 1–2 μm. Hardness HV30 1400. Coating: CVD Ti(C,N) + Al₂O₃ multi-layer. Reliable choice for machining steel and cast iron under unstable conditions.
GTWN715 (HW-K15)
Co 6.0%; WC balance; other 0.20%. Grain size 0.8–1.3 μm. Hardness HV30 1650. Uncoated carbide grade for machining aluminium and other non-ferrous metals.