Indexable drills with replaceable carbide tips
Carbide indexable drills with replaceable tips for 3×D, 4×D and 5×D depths, Ø14.0–44.0 mm.
Galtona's Indexable Drills range covers tools and inserts for indexable drilling at 3xD, 4xD, and 5xD depths, from Ø14.0 mm to Ø44.0 mm.
Designed as a performance booster for extreme machining conditions — drilling through stacks, into edges, corner angles, weld seams, and ridged surfaces — with identical internal and external indexable inserts to reduce stocking and simplify handling.
Benefits: up to 20% increase in cutting data and feed rates, optimum dimensional accuracy in difficult drilling conditions, and a single tool combining accuracy, top performance parameters, and deep drilling depths.
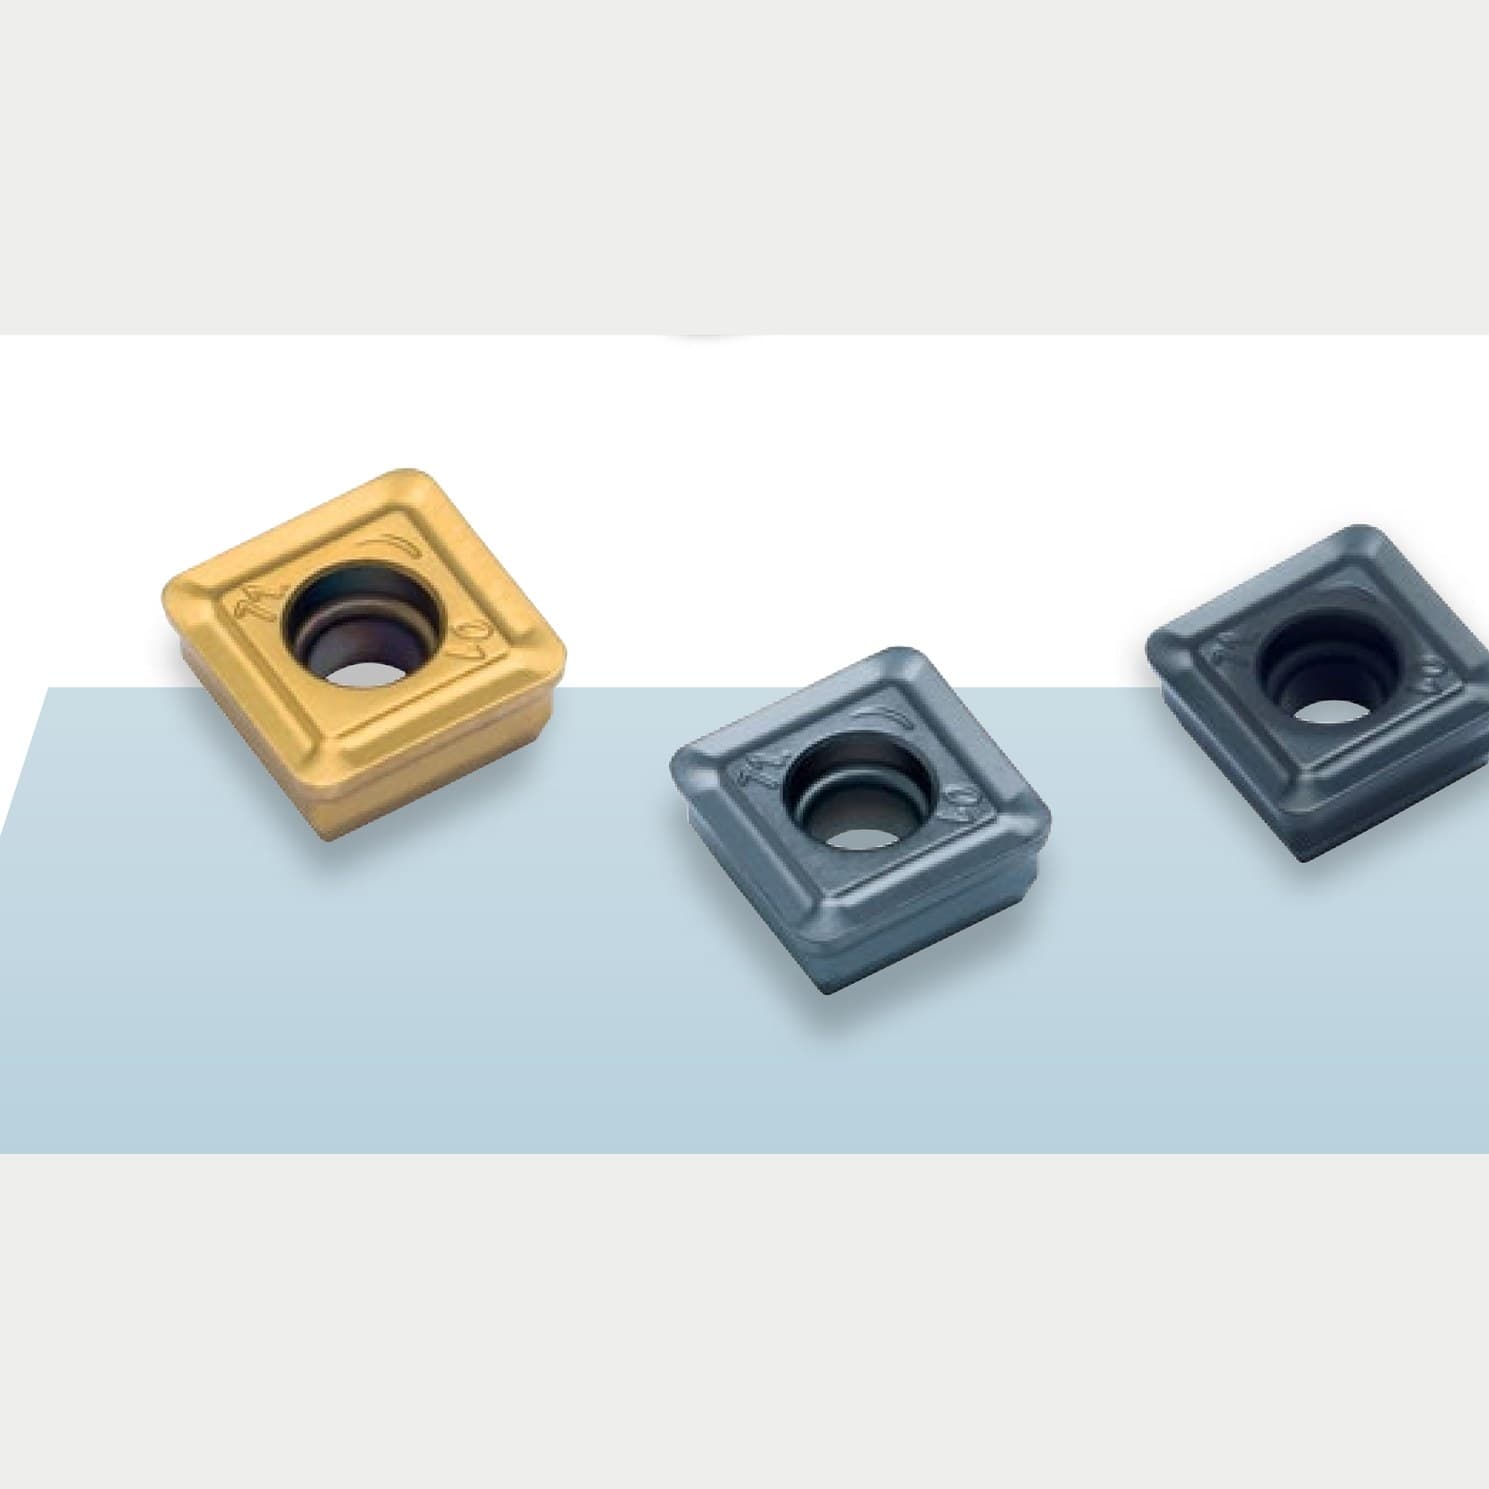
SOLT indexable inserts — steel, stainless, and cast-iron grades
SOLT Inserts, Grades & Cutting Data
Insert range by drill diameter, coating grades, and recommended cutting parameters.
All three drill lengths (3×D, 4×D, 5×D) share the same SOLT indexable insert across seven pocket sizes, selected by drill diameter via the insert-circle (IC) size below. Each pocket size is available in four chip-groove/grade combinations: …-HCD (GTPP425, steel), …-CCD (GTPK415, cast iron), …-SCD (GTPP440, stainless), and …-HCD (GTPP440, super alloys).
Insert size by drill diameter
Swipe to see more →
| Drill Ø range [mm] | Insert | IC [mm] | Corner radius [mm] |
|---|---|---|---|
| 14.0 – 16.50 | SOLT 050204 | 5.0 | 0.4 |
| 16.60 – 19.50 | SOLT 06T206 | 5.8 | 0.6 |
| 19.60 – 23.00 | SOLT 070308 | 6.9 | 0.8 |
| 23.10 – 28.00 | SOLT 080308 | 8.4 | 0.8 |
| 28.10 – 33.00 | SOLT 10T308 | 10.3 | 0.8 |
| 33.10 – 38.00 | SOLT 110408 | 11.1 | 0.8 |
| 38.10 – 44.00 | SOLT 130508 | 13.3 | 0.8 |
SOLT insert designations by pocket size (all four grades available for each)
Swipe to see more →
| Insert | …-HCD (P) GTPP425 | …-CCD (K) GTPK415 | …-SCD (M) GTPP440 | …-HCD (S) GTPP440 |
|---|---|---|---|---|
| SOLT 050204 | MM12421657 | MM12421662 | MM12421661 | MM12421660 |
| SOLT 06T206 | MM12421690 | MM12421699 | MM12421695 | MM12421693 |
| SOLT 070308 | MM12421701 | MM12421711 | MM12421704 | MM12421702 |
| SOLT 080308 | MM12421717 | MM12421752 | MM12421750 | MM12421720 |
| SOLT 10T308 | MM12421756 | MM12421772 | MM12421771 | MM12421757 |
| SOLT 110408 | MM12421773 | MM12421777 | MM12421776 | MM12421775 |
| SOLT 130508 | MM12421779 | MM12421783 | MM12421782 | MM12421780 |
Grade overview
Swipe to see more →
| Grade | ISO | Composition | Hardness | Coating | Recommended for |
|---|---|---|---|---|---|
| GTPP425 | HC-P25 / HC-M25 | Co 9.0%, mixed carbides 4.0%, WC balance, fine/medium grain | HV30 1510 | PVD TiAlN/TiN | Steel machining |
| GTPP440 | HC-M40 / HC-P40 | Co 9.0%, mixed carbides 1.4%, WC balance, submicron grain | HV30 1590 | PVD TiAlN | Austenitic steels and heat-resistant alloys |
| GTPK415 | HC-K15 | Co 6.0%, mixed carbides 2.0%, WC balance, fine grain | HV30 1630 | Uncoated | Cast iron machining |
Recommended cutting speed vc [m/min] by material group
Swipe to see more →
| Group | Material | GTPP425 vc | GTPP440 vc | GTPK415 vc |
|---|---|---|---|---|
| P | Non-alloy steels ≤500 N/mm² | 200–320 | – | – |
| P | Non-alloy/low-alloy steels 500–900 N/mm² | 250–300 | – | – |
| P | Heat-resistant/nitride/tool steels >900 N/mm² | 140–220 | – | – |
| P | High-alloy steels >900 N/mm² | 120–200 | – | – |
| P | HSS | 50–90 | – | – |
| S | Special alloys (Inconel, Hastelloy, Nimonic) | – | 20–60 | – |
| S | Titanium and titanium alloys | – | 40–60 | – |
| M | Stainless steels ≤600 N/mm² | – | 140–220 | – |
| M | Stainless steels <900 N/mm² | – | 120–200 | – |
| M | Stainless/fireproof steels >900 N/mm² | – | 120–200 | – |
| K | Grey cast iron | – | – | 160–240 |
| K | Alloy grey cast iron | – | – | 100–180 |
| K | Spheroidal graphite cast iron, ferritic | – | – | 120–160 |
| K | Spheroidal graphite cast iron, ferritic/perlitic | – | – | 100–180 |
| K | Spheroidal graphite / malleable cast iron >600 N/mm² | – | – | 90–120 |
| K | Alloyed spheroidal graphite cast iron | – | – | 90–150 |
| K | Vermicular cast iron | – | – | 70–100 |
Recommended feed f [mm/rev] by drill diameter (broad guideline — increases with diameter and decreases for finishing passes)
Swipe to see more →
| Ø14–16.5 | Ø17–19.5 | Ø20–23 | Ø23.5–28 | Ø28.5–33 | Ø33.5–38 | Ø38.5–44 |
|---|---|---|---|---|---|---|
| 0.04–0.10 | 0.08–0.10 | 0.06–0.12 | 0.06–0.12 | 0.06–0.12 | 0.06–0.12 | 0.06–0.12 |
| 0.06–0.16 | 0.10–0.16 | 0.13–0.18 | 0.13–0.20 | 0.15–0.20 | 0.15–0.20 | 0.15–0.20 |
| 0.06–0.15 | 0.10–0.15 | 0.12–0.22 | 0.14–0.22 | 0.14–0.22 | 0.14–0.22 | 0.14–0.22 |
| 0.08–0.18 | 0.10–0.18 | 0.14–0.25 | 0.18–0.30 | 0.20–0.30 | 0.20–0.30 | 0.20–0.30 |
| 0.08–0.16 | 0.10–0.16 | 0.12–0.23 | 0.16–0.28 | 0.18–0.28 | 0.18–0.28 | 0.18–0.28 |
Reduce the tabulated feed rate by 30–60% for cross-holes, stack drilling, inclined or convex entry surfaces, and by up to 50% for spot drilling in a bead or central hole.