Indexable Drills
Wendeschneidplatten-Bohrwerkzeuge für 3xD-, 4xD- und 5xD-Tiefen, Ø14.0–44.0 mm.
Das Sortiment an Wendeschneidplattenbohrern von Galtona umfasst Werkzeuge und Wendeschneidplatten für Wendeschneidplattenbohrungen in den Tiefen 3xD, 4xD und 5xD, von Ø14.0 mm bis Ø44.0 mm.
Sie wurden als Leistungssteigerung für extreme Bearbeitungsbedingungen entwickelt – beispielsweise für Bohrungen durch Materialstapel, in Kanten, Ecken, Schweißnähte und geriffelte Oberflächen. Die identischen Innen- und Außenwendeschneidplatten reduzieren den Lagerbedarf und vereinfachen die Handhabung.
Vorteile: Bis zu 20 % höhere Schnittdaten und Vorschubgeschwindigkeiten, optimale Maßgenauigkeit auch unter schwierigen Bohrbedingungen und ein einziges Werkzeug, das Genauigkeit, Spitzenleistung und große Bohrtiefen vereint.
SOLT indexable inserts — steel, stainless, and cast-iron grades
SOLT Inserts, Grades & Cutting Data
Insert range by drill diameter, coating grades, and recommended cutting parameters.
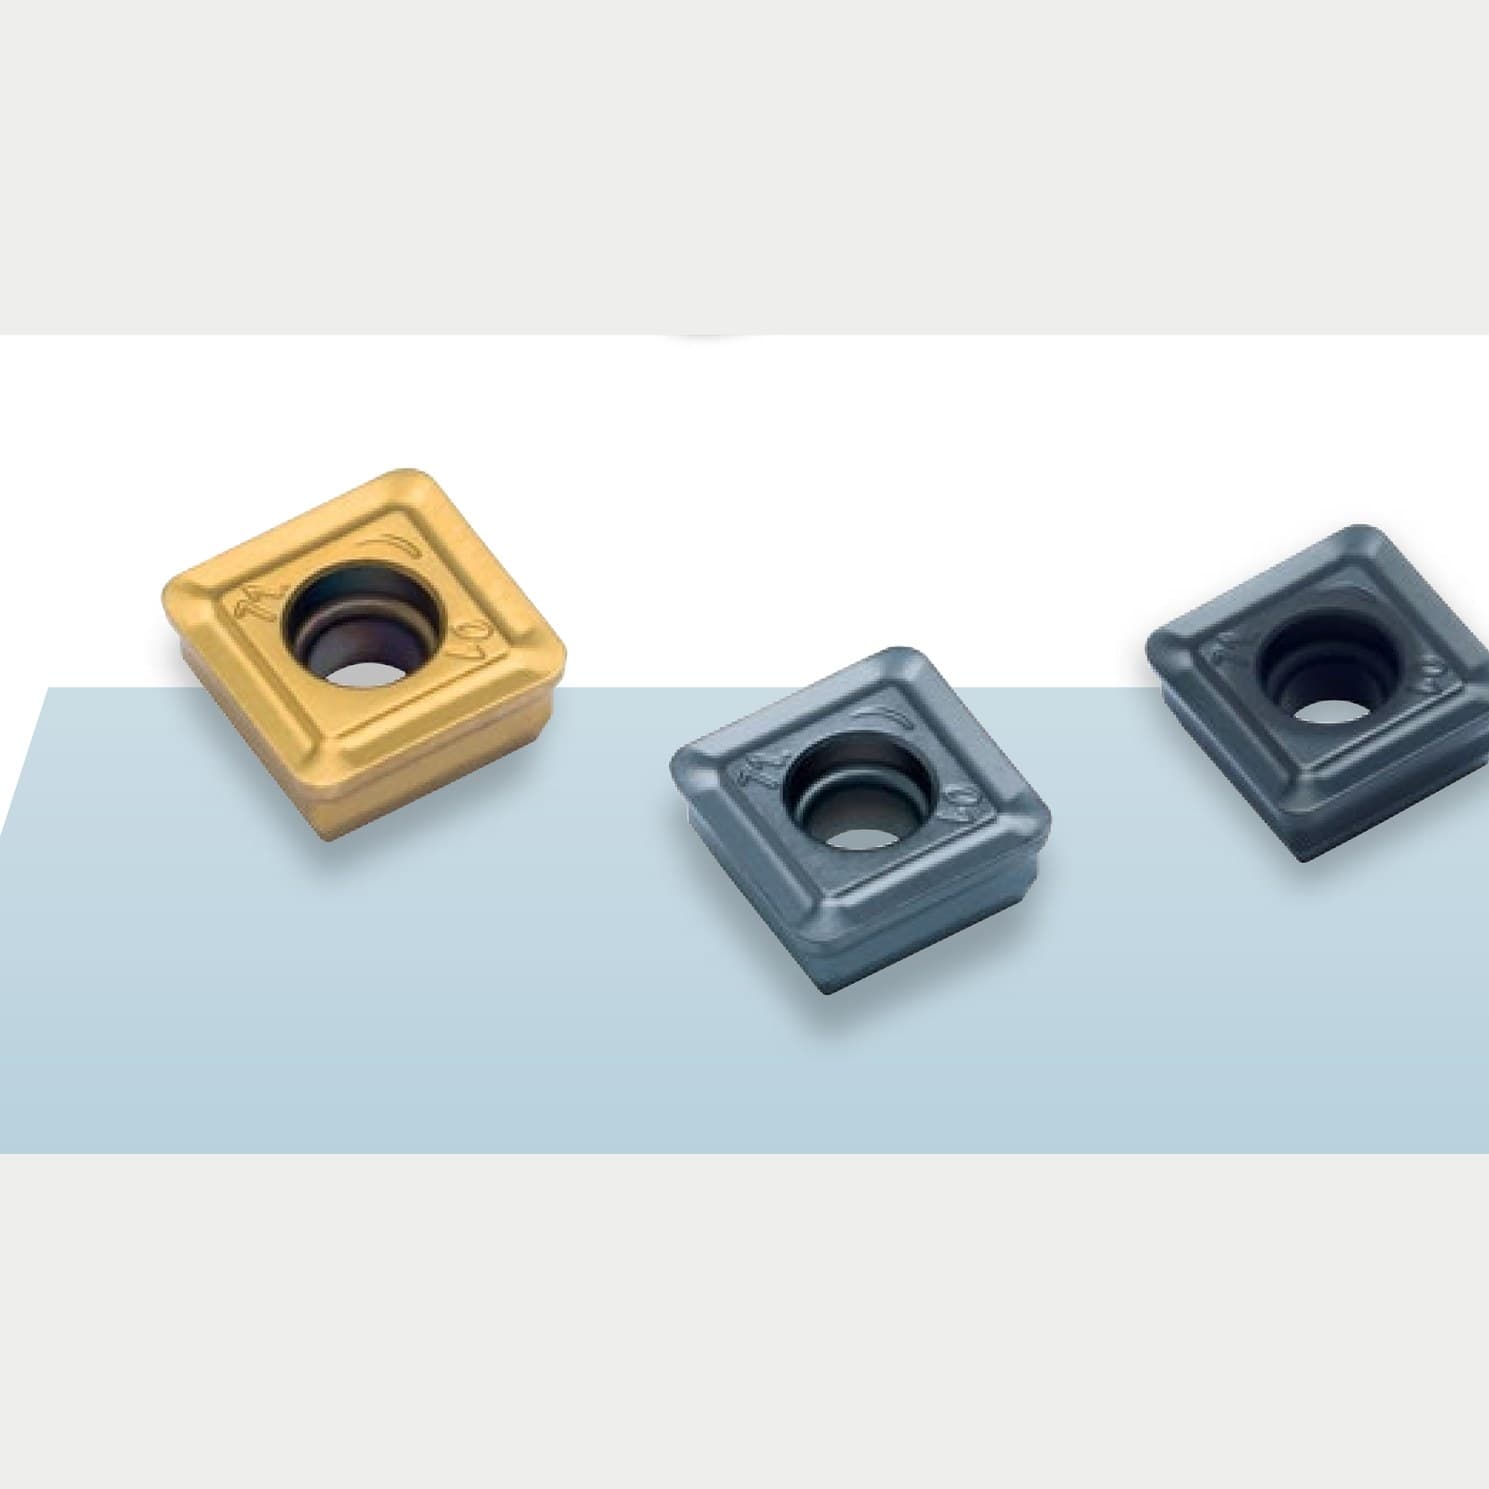
All three drill lengths (3×D, 4×D, 5×D) share the same SOLT indexable insert across seven pocket sizes, selected by drill diameter via the insert-circle (IC) size below. Each pocket size is available in four chip-groove/grade combinations: …-HCD (GTPP425, steel), …-CCD (GTPK415, cast iron), …-SCD (GTPP440, stainless), and …-HCD (GTPP440, super alloys).
Insert size by drill diameter
Swipe to see more →
| Drill Ø range [mm] | Insert | IC [mm] | Corner radius [mm] |
|---|---|---|---|
| 14.0 – 16.50 | SOLT 050204 | 5.0 | 0.4 |
| 16.60 – 19.50 | SOLT 06T206 | 5.8 | 0.6 |
| 19.60 – 23.00 | SOLT 070308 | 6.9 | 0.8 |
| 23.10 – 28.00 | SOLT 080308 | 8.4 | 0.8 |
| 28.10 – 33.00 | SOLT 10T308 | 10.3 | 0.8 |
| 33.10 – 38.00 | SOLT 110408 | 11.1 | 0.8 |
| 38.10 – 44.00 | SOLT 130508 | 13.3 | 0.8 |
SOLT insert designations by pocket size (all four grades available for each)
Swipe to see more →
| Insert | …-HCD (P) GTPP425 | …-CCD (K) GTPK415 | …-SCD (M) GTPP440 | …-HCD (S) GTPP440 |
|---|---|---|---|---|
| SOLT 050204 | MM12421657 | MM12421662 | MM12421661 | MM12421660 |
| SOLT 06T206 | MM12421690 | MM12421699 | MM12421695 | MM12421693 |
| SOLT 070308 | MM12421701 | MM12421711 | MM12421704 | MM12421702 |
| SOLT 080308 | MM12421717 | MM12421752 | MM12421750 | MM12421720 |
| SOLT 10T308 | MM12421756 | MM12421772 | MM12421771 | MM12421757 |
| SOLT 110408 | MM12421773 | MM12421777 | MM12421776 | MM12421775 |
| SOLT 130508 | MM12421779 | MM12421783 | MM12421782 | MM12421780 |
Grade overview
Swipe to see more →
| Grade | ISO | Composition | Hardness | Coating | Recommended for |
|---|---|---|---|---|---|
| GTPP425 | HC-P25 / HC-M25 | Co 9.0%, mixed carbides 4.0%, WC balance, fine/medium grain | HV30 1510 | PVD TiAlN/TiN | Steel machining |
| GTPP440 | HC-M40 / HC-P40 | Co 9.0%, mixed carbides 1.4%, WC balance, submicron grain | HV30 1590 | PVD TiAlN | Austenitic steels and heat-resistant alloys |
| GTPK415 | HC-K15 | Co 6.0%, mixed carbides 2.0%, WC balance, fine grain | HV30 1630 | Uncoated | Cast iron machining |
Recommended cutting speed vc [m/min] by material group
Swipe to see more →
| Group | Material | GTPP425 vc | GTPP440 vc | GTPK415 vc |
|---|---|---|---|---|
| P | Non-alloy steels ≤500 N/mm² | 200–320 | – | – |
| P | Non-alloy/low-alloy steels 500–900 N/mm² | 250–300 | – | – |
| P | Heat-resistant/nitride/tool steels >900 N/mm² | 140–220 | – | – |
| P | High-alloy steels >900 N/mm² | 120–200 | – | – |
| P | HSS | 50–90 | – | – |
| S | Special alloys (Inconel, Hastelloy, Nimonic) | – | 20–60 | – |
| S | Titanium and titanium alloys | – | 40–60 | – |
| M | Stainless steels ≤600 N/mm² | – | 140–220 | – |
| M | Stainless steels <900 N/mm² | – | 120–200 | – |
| M | Stainless/fireproof steels >900 N/mm² | – | 120–200 | – |
| K | Grey cast iron | – | – | 160–240 |
| K | Alloy grey cast iron | – | – | 100–180 |
| K | Spheroidal graphite cast iron, ferritic | – | – | 120–160 |
| K | Spheroidal graphite cast iron, ferritic/perlitic | – | – | 100–180 |
| K | Spheroidal graphite / malleable cast iron >600 N/mm² | – | – | 90–120 |
| K | Alloyed spheroidal graphite cast iron | – | – | 90–150 |
| K | Vermicular cast iron | – | – | 70–100 |
Recommended feed f [mm/rev] by drill diameter (broad guideline — increases with diameter and decreases for finishing passes)
Swipe to see more →
| Ø14–16.5 | Ø17–19.5 | Ø20–23 | Ø23.5–28 | Ø28.5–33 | Ø33.5–38 | Ø38.5–44 |
|---|---|---|---|---|---|---|
| 0.04–0.10 | 0.08–0.10 | 0.06–0.12 | 0.06–0.12 | 0.06–0.12 | 0.06–0.12 | 0.06–0.12 |
| 0.06–0.16 | 0.10–0.16 | 0.13–0.18 | 0.13–0.20 | 0.15–0.20 | 0.15–0.20 | 0.15–0.20 |
| 0.06–0.15 | 0.10–0.15 | 0.12–0.22 | 0.14–0.22 | 0.14–0.22 | 0.14–0.22 | 0.14–0.22 |
| 0.08–0.18 | 0.10–0.18 | 0.14–0.25 | 0.18–0.30 | 0.20–0.30 | 0.20–0.30 | 0.20–0.30 |
| 0.08–0.16 | 0.10–0.16 | 0.12–0.23 | 0.16–0.28 | 0.18–0.28 | 0.18–0.28 | 0.18–0.28 |
Reduce the tabulated feed rate by 30–60% for cross-holes, stack drilling, inclined or convex entry surfaces, and by up to 50% for spot drilling in a bead or central hole.